Syringe Manufacturing Equipment: Evaluating Throughput and Assembly Accuracy
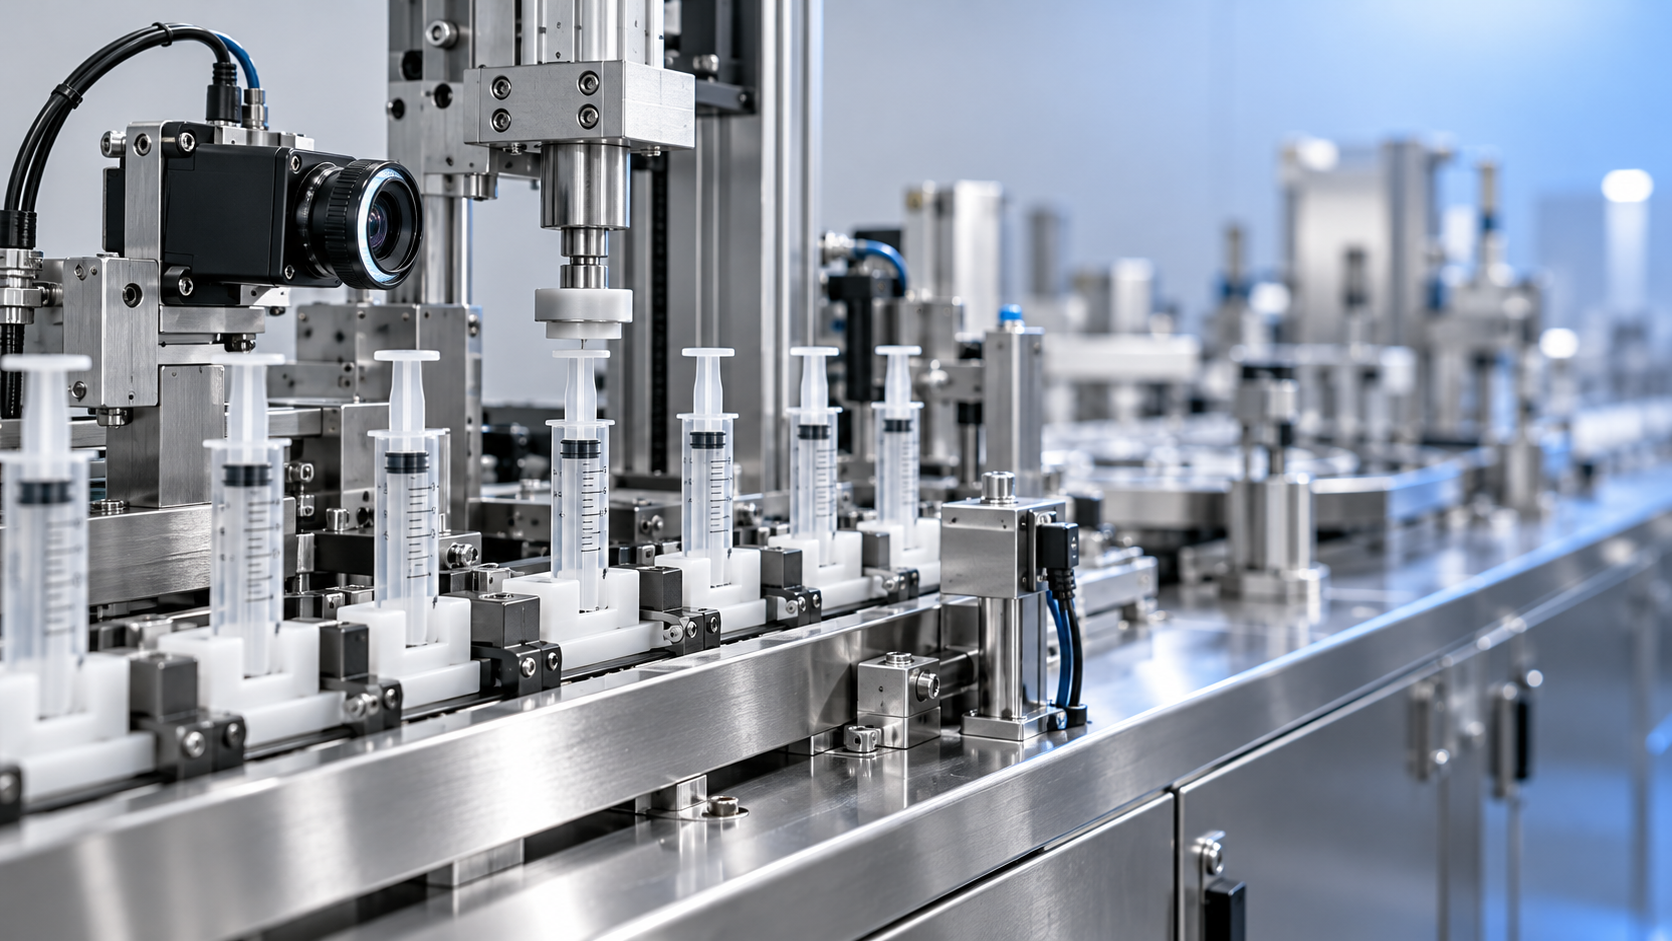
A syringe assembly line earns its capacity rating only when it produces acceptable devices at the required rate over a representative production run. For technical evaluators comparing syringe manufacturing equipment, the strongest starting point is sustained good output, supported by evidence that component alignment, insertion forces, and inspection performance remain controlled as speed increases. A higher advertised rate has limited value if stoppages, rejected assemblies, or undetected defects consume the apparent advantage.
The right choice depends on the syringe design, incoming component variation, and the production schedule. A dedicated line running one configuration faces a different challenge from equipment expected to switch between barrel sizes, plunger designs, or needle arrangements. Before comparing quotations, define the product family and the exact process boundary: molded components entering assembly, completed syringes leaving inspection, or packaged units ready for a subsequent process. Those boundaries determine whether two capacity claims are comparable.
Establish a common basis for throughput. Ask each supplier to distinguish its maximum mechanical cycling rate, demonstrated running rate, and accepted output over scheduled production time. Mechanical speed describes how quickly a mechanism can move under specified conditions. It does not establish how consistently the complete line can feed components, assemble them correctly, identify defects, and discharge acceptable product.
Two measures help expose that difference. Running good output is the number of accepted units produced per unit of actual operating time. Scheduled good output divides accepted units by the full evaluation period, including the stops and interventions assigned to that period. Record both. The first helps assess assembly performance at speed; the second shows whether the equipment can support a production commitment.
For illustration, suppose a line runs at 300 assemblies per minute, operates for 85% of a scheduled hour, and accepts 98% of the units it processes. Its scheduled good output would be approximately 250 units per minute. These are hypothetical figures, but the calculation demonstrates why nominal speed alone can mislead. If a supplier presents an overall efficiency figure, request its definitions and underlying records before using it in a capacity model.
Keep first-pass yield separate from eventual acceptance. A unit that passes only after adjustment or rework consumes additional capacity and handling. Define first-pass yield as the share of units entering the agreed process that complete it successfully without rework, and state how startup scrap, setup pieces, and units removed during interruptions are counted. Otherwise, an attractive yield percentage may exclude losses that the production team will have to absorb.
Capacity planning should also account for what happens beyond assembly. If packaging repeatedly stops the line, or component supply cannot replenish feeders at the required rate, assembly speed cannot become finished output. Identify which interfaces belong in the trial and which require separate evidence. An isolated machine demonstration can establish a useful capability, but its result should retain that boundary when translated into a factory production forecast.
Translate assembly accuracy into device performance. Positional repeatability is useful, but it is only one part of accuracy. The evaluator needs to know whether components are correctly oriented, fully seated, retained as intended, and assembled without damage. The relevant characteristics differ between a conventional disposable syringe, a safety syringe, and a system involving a prefilled barrel. Acceptance criteria must follow the actual design and its intended use.
For a barrel-and-plunger assembly, examine how the equipment controls alignment and insertion depth, and whether insertion can damage the stopper or barrel. Where the process assembles a stopper to a plunger rod, verify that attachment as a separate operation. Where needle, hub, cap, or safety components are included, evaluate their seating and engagement independently. A finished assembly can look correct while retaining a functional defect that external vision cannot reliably identify.
Force and displacement monitoring can provide useful evidence during insertion or engagement. An unexpected force profile may indicate interference, a missing component, misalignment, or a seating problem. However, a force threshold becomes meaningful only after it has been related to acceptable and defective assemblies. Ask how the monitoring limits were developed and whether permitted changes in component dimensions or material behavior could shift the signal enough to cause missed defects or unnecessary rejects.
Distinguish machine repeatability from process capability. A mechanism may return accurately to its programmed position while the component sits inconsistently in its fixture. Nest wear, contamination, barrel ovality, component temperature, and feeder orientation can all affect the resulting assembly. Capability evidence should therefore address the finished characteristic and an adequate measurement method, with the product range and operating conditions clearly identified.
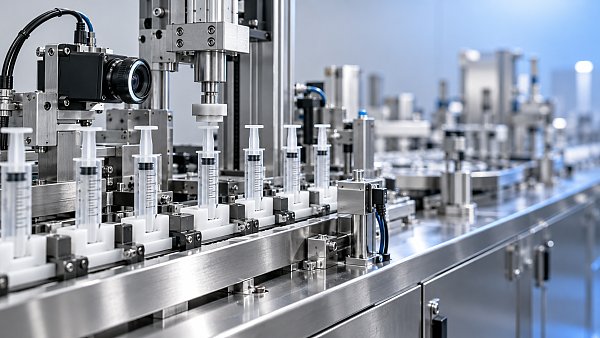
Inspect the relationship between locating, assembly, and verification. Each critical operation needs a controlled component position, an assembly method suited to the permitted variation, and an inspection method capable of detecting the relevant failure. Where one fixture carries a component through several stations, assess whether a locating error can persist through the sequence. Where components transfer between fixtures, examine the additional opportunities for movement or damage.
Increasing speed puts pressure on this relationship. Shorter cycle times leave less time for components to settle, insertion motions to complete, and inspection systems to acquire usable information. Faster feeder delivery can also change how parts arrive at the assembly station. Request evidence at the proposed production rate, including defect categories and process measurements. A low-speed demonstration establishes little about accuracy at a substantially higher operating rate.
Test inspection as part of the production process. A low reject rate can reflect a capable assembly process, weak detection, or permissive inspection limits. A high reject rate may indicate assembly problems, incoming component variation, or excessive false rejection. Neither figure is interpretable without knowing what the inspection system can detect and how its decisions were checked.
Use controlled defect challenges to evaluate that capability. The challenge set should represent credible failures for the design: missing or reversed components, incomplete seating, damaged features, and other relevant assembly faults. Include examples near the acceptance boundary where feasible. Obvious defects alone provide little evidence that a system can discriminate between acceptable variation and a subtle functional problem.
The challenge should verify the complete rejection sequence. Detection must connect to the correct unit, the reject mechanism must remove it, and the equipment must confirm successful segregation or respond appropriately when removal fails. Check what happens after a stop, restart, jam clearance, or loss of tracking. Correct inspection results have limited value if the line loses the association between a result and the physical assembly.
Some characteristics require functional testing or destructive examination, which limits how extensively they can be checked during production. Define which attributes receive continuous monitoring and which require sampling. External vision, for example, cannot establish every aspect of seal integrity or plunger movement. Where equipment signals are used to infer a functional result, request evidence of that relationship and understand the conditions under which it remains valid.
Make the equipment trial represent the proposed operating envelope. A useful trial includes the target product, target rate, representative components, and enough operating time to expose replenishment, interruptions, and recovery behavior. The necessary duration depends on process risk and the production pattern. A brief run with carefully selected components may show that the mechanism works while leaving sustained production capability unresolved.
Agree on the trial protocol before accepting performance claims. It should establish:
- The product configurations, component specifications, and component lots included in the evaluation.
- The speed settings, scheduled trial duration, and rules for counting downtime, scrap, rework, and accepted units.
- The assembly characteristics to measure, their acceptance limits, and the suitability of the measurement methods.
- The defect challenges, independent verification checks, and criteria for evaluating rejection performance.
- The replenishment, stop-and-restart, changeover, and recovery activities included in the demonstration.
Component selection deserves particular attention. A line demonstrated with one narrow set of dimensions may perform differently when supplied with components elsewhere within the approved tolerance range. Where feasible, include multiple lots and relevant dimensional variation. If only one lot is available, record that limitation and plan further qualification before treating the result as evidence for the full supply specification.
Review performance at startup, during stable running, and after interruptions separately. An average can conceal a repeated loss of control during restart or feeder replenishment. Time-stamped event logs, defect counts by station, intervention records, and measurements of critical characteristics help identify these patterns. Video can clarify a mechanical event, but it should support the production records rather than substitute for them.
A short stop can be especially revealing. Does the equipment preserve component position and tracking? What happens to partially assembled units? Can an operator resume production through a defined sequence, or does recovery depend on manual judgment? Frequent brief interventions can erode capacity even when no individual breakdown appears serious. Include their full recovery time in the output assessment.
For multiple product configurations, measure changeover from the last acceptable unit of one product to stable acceptable production of the next. Tool replacement is only part of that interval. Feeder adjustment, recipe loading, inspection setup, clearance checks, and startup losses may determine the practical cost. Verify how settings and tooling prevent an incompatible configuration from running, particularly where parts look similar but have different assembly requirements.
Use the evidence to define the purchase commitment. A technically useful quotation should state the configurations covered, component requirements, demonstrated speed, accepted output, and quality criteria under specified operating conditions. It should identify the inspection functions included and distinguish them from characteristics requiring separate verification. This makes performance review concrete and prevents a broad capacity statement from carrying assumptions that were never tested.
Factory acceptance and site acceptance should address different uncertainties. The factory trial can demonstrate the supplied machine and its controls under agreed conditions. Site testing establishes performance with the installation’s utilities, material handling, operators, and connected processes. Establish which criteria apply at each stage and how unresolved deviations will be handled before the equipment ships.
Finally, compare the cost per acceptable unit using defensible assumptions for downtime, rejects, changeovers, labor, tooling, and maintenance. A faster line may justify its price when it sustains higher good output across the required product range. A lower-speed line may be the stronger choice when it recovers predictably and maintains assembly control with less intervention. The purchase decision should rest on an operating envelope demonstrated with representative components—and an acceptance specification that preserves those conditions when the equipment reaches the production floor.
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
 Oct 22, 2026Mitsubishi Electric Develops Industry-First Humanoid Robot–CNC Machining SystemMitsubishi Electric Develops Industry-First Humanoid Robot–CNC Machining System
 Oct 22, 2026Aerospace Aluminum Machining: How to Control Distortion in Thin-Wall PartsAerospace Aluminum Machining: How to Control Distortion in Thin-Wall Parts
 Oct 21, 2026Genesis Energy commissions 200 MWh battery storage system at HuntlyGenesis Energy commissions 200 MWh battery storage system at Huntly
 Oct 21, 2026Buying AMI Smart Meters Wholesale: Compatibility Checks and Total CostsBuying AMI Smart Meters Wholesale: Compatibility Checks and Total Costs
 Oct 20, 2026Werner Enterprises Issues Q3 Earnings Warning as Costs RiseWerner Enterprises Issues Q3 Earnings Warning as Costs Rise
 Oct 20, 2026Are Digital Twins Viable for SMEs? Costs, Use Cases, and Data RequirementsAre Digital Twins Viable for SMEs? Costs, Use Cases, and Data Requirements
 Oct 19, 2026Choosing a Wholesale Servo Motor Exporter: Traceability and Warranty ChecksChoosing a Wholesale Servo Motor Exporter: Traceability and Warranty Checks
 Oct 18, 2026Syringe Manufacturing Equipment: Evaluating Throughput and Assembly AccuracySyringe Manufacturing Equipment: Evaluating Throughput and Assembly Accuracy
 Oct 17, 2026Air Freight Forwarding Services: How to Compare Quotes for Urgent ShipmentsAir Freight Forwarding Services: How to Compare Quotes for Urgent Shipments
 Oct 16, 2026Wholesale Solar Panels: How to Compare Bulk Quotes by Total Landed CostWholesale Solar Panels: How to Compare Bulk Quotes by Total Landed Cost
 Oct 15, 2026Supply Chain Intelligence for Sourcing: How to Vet New SuppliersSupply Chain Intelligence for Sourcing: How to Vet New Suppliers
 Oct 14, 2026How skills shortages slow smart manufacturing in Southeast AsiaHow skills shortages slow smart manufacturing in Southeast Asia
 Oct 14, 2026How CNC wire-cut machining maintains tight tolerances in thick partsHow CNC wire-cut machining maintains tight tolerances in thick parts
 Oct 14, 2026Can automated feeding stabilize metal forming in smart factories?Can automated feeding stabilize metal forming in smart factories?
 Oct 14, 2026Can CT inspection detect internal defects in metal additive parts?Can CT inspection detect internal defects in metal additive parts?
 Oct 14, 2026When does additive manufacturing reduce lead time for spare parts?When does additive manufacturing reduce lead time for spare parts?
 Oct 14, 2026How production volume affects ROI on an automated painting lineHow production volume affects ROI on an automated painting line
 Oct 14, 2026What data does manufacturing bottleneck analysis consulting need?What data does manufacturing bottleneck analysis consulting need?
 Oct 14, 2026When should you hire a consultant for manufacturing bottlenecks?When should you hire a consultant for manufacturing bottlenecks?
 Oct 14, 2026How Do You Measure AI Adoption Maturity in a Traditional Factory?How Do You Measure AI Adoption Maturity in a Traditional Factory?
 Oct 14, 2026Are Chinese AI-Assisted Surgical Devices Gaining Global Trust?Are Chinese AI-Assisted Surgical Devices Gaining Global Trust?
 Oct 14, 2026What Happens When Warehouse Robots Need Software Updates Mid-Operation?What Happens When Warehouse Robots Need Software Updates Mid-Operation?
 Oct 14, 2026How Do Plants Calculate Real Savings from Energy-Efficient Equipment?How Do Plants Calculate Real Savings from Energy-Efficient Equipment?
 Oct 14, 2026Are Digital Twins Only for Large Enterprises, or Can SMEs Use Them?Are Digital Twins Only for Large Enterprises, or Can SMEs Use Them?
 Oct 14, 2026What Are the Common Failure Modes in Legacy Industrial Control Systems?What Are the Common Failure Modes in Legacy Industrial Control Systems?
 Oct 14, 2026Do Electronic Component Distributors Add Value or Just Markup?Do Electronic Component Distributors Add Value or Just Markup?
 Oct 14, 2026What ESG Requirements Apply to Solar PV Exporters Selling to Europe?What ESG Requirements Apply to Solar PV Exporters Selling to Europe?