Choosing Carbon Steel Grades for OEM Machined Parts: Key Factors
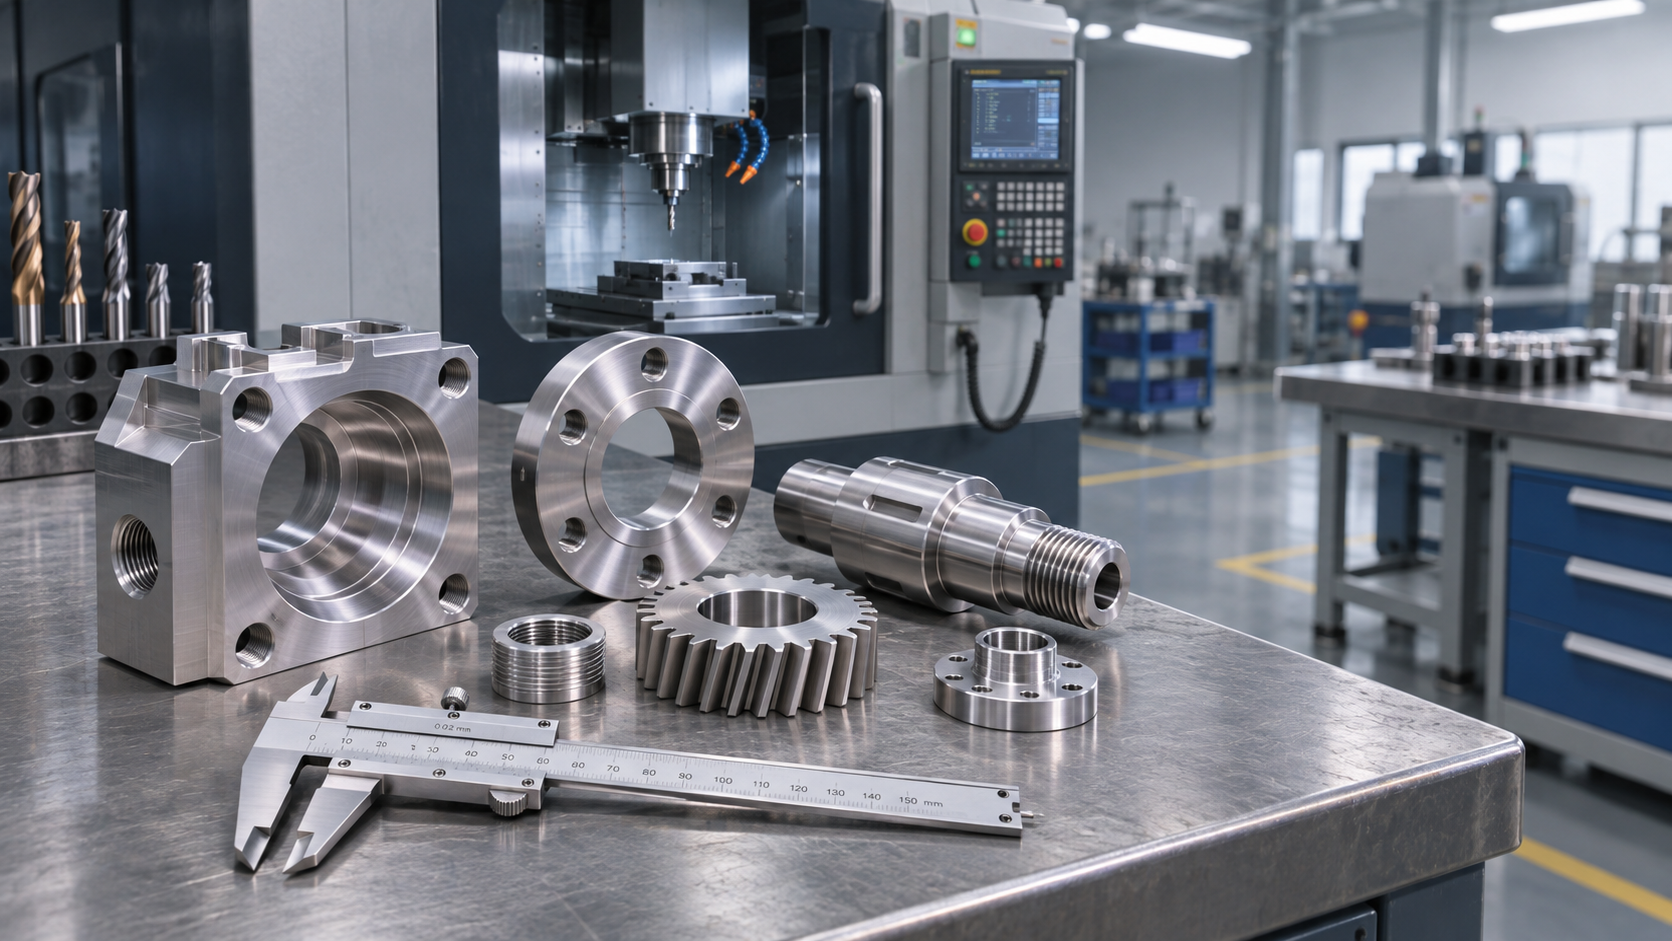
The right grade for OEM machined parts in carbon steel is the one that meets the finished component’s mechanical and service requirements at an acceptable manufacturing cost—not simply the grade with the highest strength or lowest bar price. Low-carbon steels favor forming and welding; medium-carbon steels offer a stronger basis for heat treatment; and free-machining grades can reduce cutting effort but introduce trade-offs in weldability, ductility, or cleanliness.
Grade selection must be tied to the material condition, section size, manufacturing sequence, and acceptance tests. A designation alone does not guarantee the hardness, fatigue performance, surface integrity, or dimensional stability of the finished part.
Comparing carbon steel grades for OEM machined parts
Common SAE/AISI designations provide a useful starting point, but the purchase specification should also identify the applicable material standard, product form, and delivery condition. The comparisons below describe general tendencies rather than guaranteed properties.
These grades are not interchangeable by carbon percentage alone. Sulfur, phosphorus, lead, manufacturing route, and delivery condition affect machining and performance. Even within one grade, cold-drawn bar and hot-rolled bar can behave differently during machining because their dimensions, surface condition, strength, and residual stresses differ.
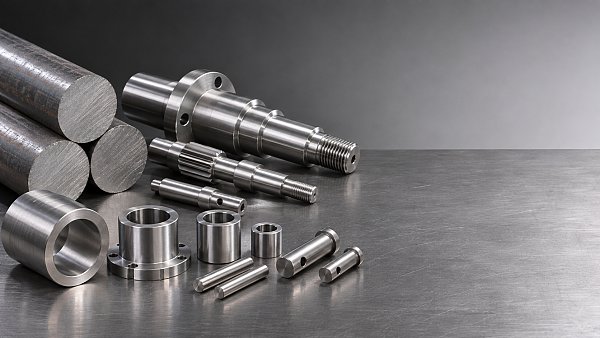
Start with the failure mode, not the grade
Define the load case before selecting a material: maximum and cyclic loads, load direction, impact, contact pressure, temperature, and the consequences of failure. A shaft limited by fatigue may require a different material and process route from a similarly sized spacer loaded mainly in compression.
- Yielding or permanent deformation: Specify the required mechanical properties in the finished condition and assess the critical section, not only the nominal material designation.
- Fatigue: Evaluate stress concentrations, surface finish, inclusions, residual stress, and heat-treatment effects alongside strength. A harder part is not automatically a more fatigue-resistant part.
- Surface wear: Determine whether the part needs a hard surface with a tougher core or a hardness requirement throughout the section.
- Impact or shock: Consider toughness at the operating temperature and validate it in the specified condition; high hardness can compromise resistance to brittle failure.
- Corrosion: Carbon steel grades generally require a suitable protective system in corrosive service. Increasing carbon content is not a substitute for corrosion-resistant material or effective coating design.
Geometry changes the decision. A slender component with a tight straightness requirement is particularly sensitive to stress relief and machining sequence, while a thick section may not achieve the same hardened structure at its center as a small test piece. Where a joint is welded, assess the full assembly process rather than choosing solely on the basis of the machined component.
Choose the heat-treatment route with the section size in mind
Carbon content influences the hardness that can be achieved, but hardenability—the ability to harden to a given depth—is a separate consideration. Quench severity, part diameter, chemistry, and initial microstructure all affect the result. A 1045 component may respond well to quenching and tempering in a suitable section, yet a larger section may develop substantially different properties between surface and core.
Case hardening for surface wear and a tougher core
Low-carbon grades such as 1018 or 1020 can be considered for carburizing when the design calls for a hard, wear-resistant surface and a comparatively tough core. The drawing should distinguish effective case depth from total case depth, identify the measurement method, and specify the hardness range and locations.
Carburizing adds processing time and introduces distortion risk. Allowances for grinding or other finishing operations may be needed, and sharp corners or abrupt section changes deserve attention because they can concentrate stress during service and heat treatment.
Through-hardening and tempering for bulk properties
Medium-carbon steel such as 1045 is a candidate when the part needs greater bulk strength than a low-carbon grade can provide. Specify the required finished hardness or mechanical properties together with test locations; do not assume that a heat-treatment instruction alone establishes uniform properties through every section.
Higher-carbon grades can achieve higher hardness, but the associated loss of toughness and increased risk of cracking or distortion can make them unsuitable for shock-loaded or intricate components. If a carbon steel cannot meet the required combination of hardenability, toughness, and section size, consider whether an alloy steel or a different component design is warranted.
Machinability is a process outcome, not a material-only rating
Free-machining steels can improve chip control and support productive turning, especially where a part has many small features and high production volume. Resulfurized grades contain inclusions that assist chip breaking, while lead additions in grades such as 12L14 improve machinability. Those benefits must be weighed against directional properties, service loads, joining requirements, and applicable material restrictions.
For a welded component, a low-carbon grade may be a better starting point than a free-machining grade, although weld procedure, thickness, restraint, and service requirements still control the outcome. For a fatigue-critical shaft, improved cycle time should not override evaluation of inclusions, surface condition, and the required qualification tests.
Machining cost also depends on stock condition, tooling, coolant, feature geometry, and the amount of material removed. Comparing two grades on quoted cycle time alone can conceal additional costs for heat treatment, finishing, inspection, scrap, or restricted supplier availability.
Control distortion through the manufacturing sequence
Residual stress can be present in supplied stock and can also arise during cutting and heat treatment. Removing material unevenly may release those stresses, causing a thin wall to move or a long shaft to bend. Tight tolerances therefore require an agreed process sequence, not merely a precise final inspection.
A route for a heat-treated shaft might include rough machining with sufficient stock allowance, heat treatment, straightening if permitted, and finish grinding of critical diameters. Whether intermediate stress relief is appropriate depends on the steel, incoming condition, geometry, and process; its temperature and timing must be compatible with the required final properties.
Identify dimensions that apply after heat treatment and surface finishing. Coating thickness, grinding stock, bore distortion, and thread condition can each affect assembly. If a surface-hardened part needs a precise bore or bearing seat, establish which surfaces will be finished after hardening and how the required case depth will be maintained.
Use a hypothetical comparison to expose the trade-offs
Consider a hypothetical turned pin that carries repeated contact loads, fits into a close-tolerance bore, and must resist surface wear. A low-carbon grade with carburizing could provide a hard case and a tougher core, but the route adds heat-treatment distortion and may require finish grinding. A 1045 pin could offer a different balance through quenching and tempering or an appropriate surface-hardening process, subject to section size and the required wear depth.
A free-machining grade might reduce turning cost, but that advantage is not sufficient if fatigue, contact loading, or joining requirements cannot be demonstrated. The decision should compare finished-part performance and process capability, including the cost of achieving the bore fit after treatment—not only the purchase price of bar stock.
Turn the chosen grade into an inspectable specification
A drawing that states only “1045 steel” leaves important variables unresolved. The specification should connect the material order to the finished component and make clear which requirements apply before and after processing.
- Material identity: State the grade, applicable standard and revision, product form, and permitted substitutions.
- Incoming condition: Define hot-rolled, cold-drawn, annealed, normalized, or other required condition, as applicable.
- Finished properties: Set mechanical-property or hardness limits, test locations, and test methods appropriate to the part.
- Heat treatment: Specify the required result, including case depth and core requirements where relevant; identify any process controls that must be agreed.
- Geometry and surface: Define tolerances, surface finish, critical radii, permissible distortion, and the condition in which dimensions are checked.
- Verification and traceability: Require appropriate material certificates, heat identification, inspection records, and retention of traceability through subcontracted processes.
For cross-border sourcing, treat equivalent grade designations as candidates for review rather than automatic substitutions. Compare the applicable chemistry limits, product standard, delivery condition, dimensional requirements, and required properties; approve any change through the same engineering and validation process used for the original specification.
Make the final decision on qualified total cost
Compare candidate materials across the complete route: stock availability, machining, heat treatment, finishing, inspection, expected yield, and qualification. A cheaper grade is not economical if it needs extensive rework to hold tolerance; a more machinable grade is not appropriate if its finished properties cannot meet the load case.
Before release, confirm that representative parts made from the proposed stock and process route satisfy the critical dimensions and performance requirements. The defensible selection is the grade and manufacturing condition that can be specified, produced, inspected, and supplied consistently for the intended service.
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
 Nov 22, 2026Golmud's 60 MW Liquid Air Storage Project Uses Fully Domestic EquipmentGolmud's 60 MW Liquid Air Storage Project Uses Fully Domestic Equipment
 Nov 22, 2026Precision Engineering for Medical Devices: Tolerances and MaterialsPrecision Engineering for Medical Devices: Tolerances and Materials
 Nov 21, 2026EDF Acquires 1GWh Holloway Battery Storage Project in AustraliaEDF Acquires 1GWh Holloway Battery Storage Project in Australia
 Nov 21, 2026Choosing Carbon Steel Grades for OEM Machined Parts: Key FactorsChoosing Carbon Steel Grades for OEM Machined Parts: Key Factors
 Nov 20, 2026China’s First Virtual Power Plant Report Says Capacity Target Met EarlyChina’s First Virtual Power Plant Report Says Capacity Target Met Early
 Nov 20, 2026Choosing an OEM Heavy Equipment Manufacturer: Capabilities and Quality ChecksChoosing an OEM Heavy Equipment Manufacturer: Capabilities and Quality Checks
 Nov 19, 2026India Adds Record 8.4 GW of Open-Access Solar in First Nine Months of 2026India Adds Record 8.4 GW of Open-Access Solar in First Nine Months of 2026
 Nov 19, 2026B2B Intelligence for Green Energy: Finding New Market OpportunitiesB2B Intelligence for Green Energy: Finding New Market Opportunities
 Nov 18, 2026Global Solar Additions Hit Record in 2025, Forecast to Fall in 2026Global Solar Additions Hit Record in 2025, Forecast to Fall in 2026
 Nov 18, 2026Supply Chain Visibility for Supplier Management: How to Spot Delivery RisksSupply Chain Visibility for Supplier Management: How to Spot Delivery Risks
 Nov 17, 2026US Battery Storage Deployment Tops 200 GWh; 74 GWh Forecast for 2026US Battery Storage Deployment Tops 200 GWh; 74 GWh Forecast for 2026
 Nov 17, 2026Choosing a Solar Tracker for Ground-Mount PV: Site and Design FactorsChoosing a Solar Tracker for Ground-Mount PV: Site and Design Factors
 Nov 16, 2026US Polysilicon and Solar Product Tariffs and Import Price Floor Take Effect December 4US Polysilicon and Solar Product Tariffs and Import Price Floor Take Effect December 4
 Nov 16, 2026How Industrial Buyers Can Evaluate B2B Intelligence Reports on SuppliersHow Industrial Buyers Can Evaluate B2B Intelligence Reports on Suppliers
 Nov 15, 2026CATL Sets Tener Sodium Delivery Timeline, Targeting LFP on CostCATL Sets Tener Sodium Delivery Timeline, Targeting LFP on Cost
 Nov 15, 2026Electric Wheelchairs for Disabled Adults: Choosing the Right Fit and RangeElectric Wheelchairs for Disabled Adults: Choosing the Right Fit and Range
 Nov 14, 2026China Expects Clean Energy to Meet All New Electricity Demand by 2030China Expects Clean Energy to Meet All New Electricity Demand by 2030
 Nov 14, 2026Choosing a Digital X-Ray Detector Supplier: Compatibility and SupportChoosing a Digital X-Ray Detector Supplier: Compatibility and Support
 Nov 13, 2026Ecuador Sets Zero VAT and Currency Outflow Tax Rates for Solar and Storage EquipmentEcuador Sets Zero VAT and Currency Outflow Tax Rates for Solar and Storage Equipment
 Nov 13, 2026Choosing an OEM Machined Parts Manufacturer: Quality, Capacity and Lead TimesChoosing an OEM Machined Parts Manufacturer: Quality, Capacity and Lead Times
 Nov 12, 2026South Africa Registers 2 GW of New Solar PV Capacity in Q3 2026South Africa Registers 2 GW of New Solar PV Capacity in Q3 2026
 Nov 12, 2026Mexico Supply Chain Market Research: Nearshoring Opportunities and RisksMexico Supply Chain Market Research: Nearshoring Opportunities and Risks
 Nov 11, 2026US Senate Advances Bipartisan BAAJA Energy Permitting BillUS Senate Advances Bipartisan BAAJA Energy Permitting Bill
 Nov 11, 2026Inventory Management Decision Support: When and How Much to ReorderInventory Management Decision Support: When and How Much to Reorder
 Nov 10, 2026China's Trade Surplus Tops $1 Trillion Through October as Exports Rise 35.2%China's Trade Surplus Tops $1 Trillion Through October as Exports Rise 35.2%
 Nov 10, 2026Choosing Surgical PPE: Gowns, Gloves, Masks and Eye ProtectionChoosing Surgical PPE: Gowns, Gloves, Masks and Eye Protection
 Nov 09, 2026US Solar Imports Shift as Domestic Manufacturing Investment Reshapes Global TradeUS Solar Imports Shift as Domestic Manufacturing Investment Reshapes Global Trade