Inventory Management Decision Support: When and How Much to Reorder
Knowing when and how much to reorder is essential to keeping operations running without tying up excess capital in stock. Inventory management decision support turns demand patterns, supplier lead times, safety stock, and ordering costs into purchasing recommendations. The useful question is not whether a system can produce a number, but whether the operator can see what that number assumes and act before a shortage becomes urgent.
A reorder point answers when to replenish. An order quantity answers how much to buy. Both depend on the same operational reality: what is available, what is already committed, when incoming stock can actually be used, and how demand may change before it arrives.
Start with inventory position, not the shelf count
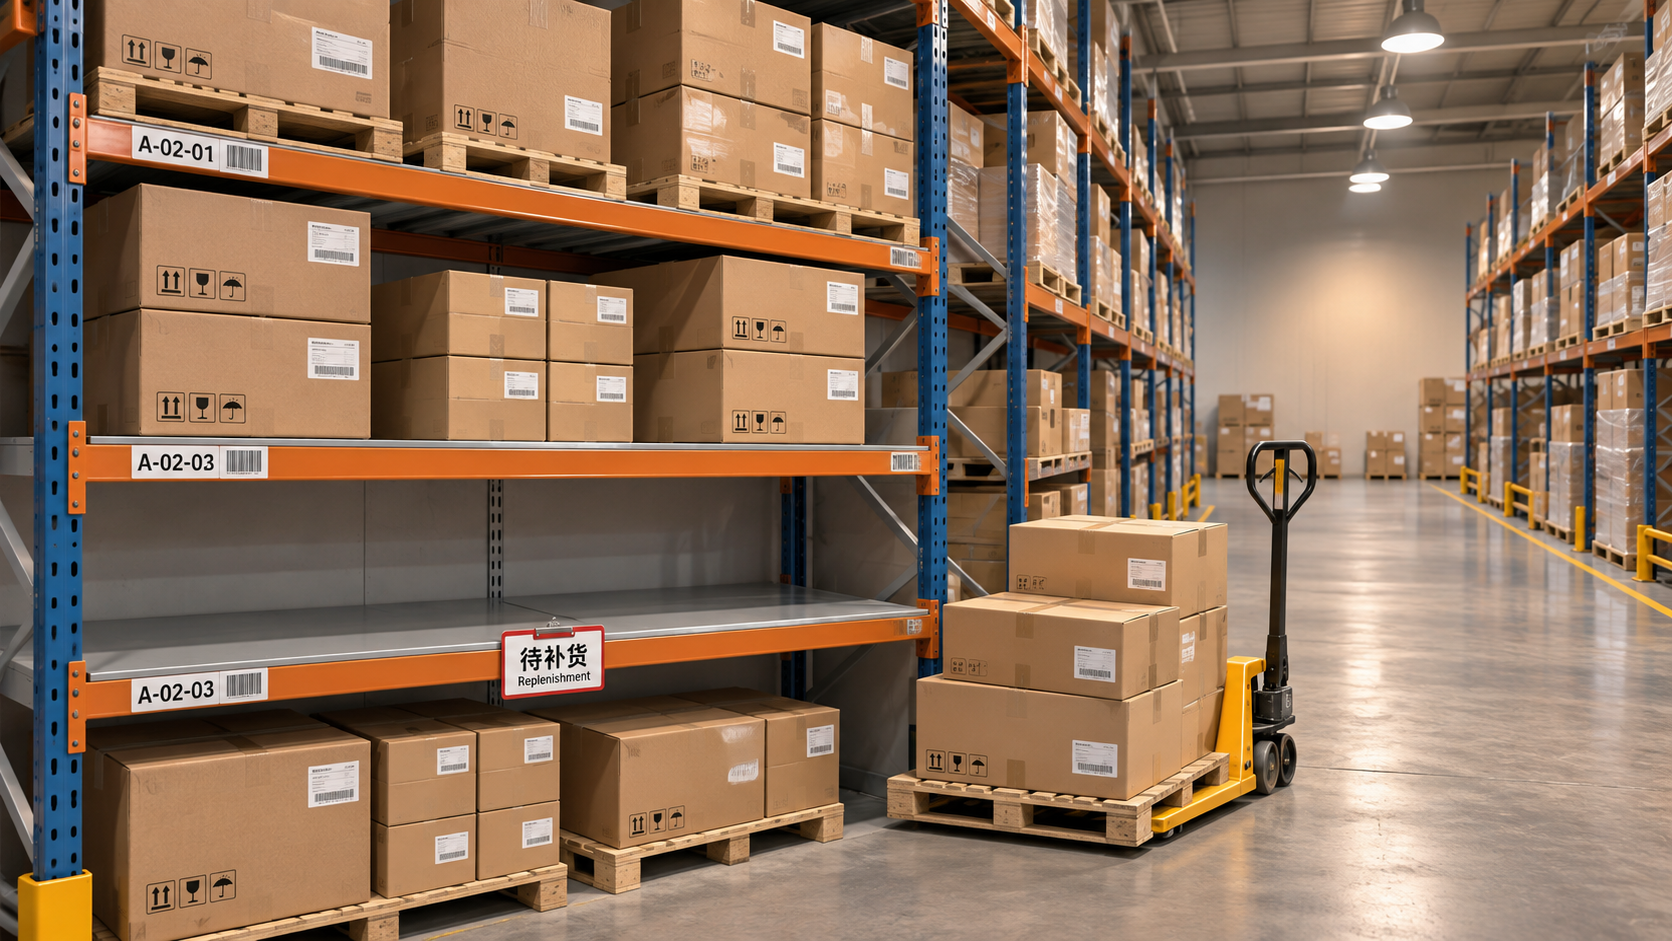
A warehouse may show 500 units on hand, but that figure alone is not enough to decide whether to order. Some units may already be allocated to customer orders or production jobs. Others may be damaged, quarantined, or approaching expiry. Meanwhile, an open purchase order may be scheduled to arrive next week—or may be overdue.
Inventory position = usable on-hand stock + reliable incoming stock − committed demand.
The exact calculation depends on how the inventory system records allocations and backorders. The key is consistency: subtract each commitment once, not twice. Incoming stock should also be assessed by date and reliability. A purchase order with an unconfirmed delivery date is not equivalent to material already received and released for use.
For items managed across multiple locations, calculate the position at the level where stock is actually consumed. A surplus in one warehouse will not prevent a stockout elsewhere unless it can be transferred in time and the transfer is operationally feasible.
Set a reorder point that reflects the real replenishment time
A basic reorder point combines expected demand during replenishment with a safety-stock buffer:
Reorder point = average demand per day × replenishment lead time in days + safety stock.
Use compatible time units. If demand is measured per working day, lead time must also be expressed in working days. More importantly, define lead time from the moment the organization needs to place an order until the stock is available for use—not merely the supplier’s quoted production time. Internal approval, transport, receiving, inspection, and put-away can all affect that interval.
Consider an illustrative component with average demand of 20 units per day, a 10-day replenishment lead time, and safety stock of 60 units. Its reorder point is 260 units: 200 units for expected demand during lead time, plus the buffer. Under continuous review, the operator should trigger replenishment when inventory position reaches or falls below 260 units.
That trigger is not a guarantee against shortages. If a large order arrives suddenly, inventory position can fall well below the threshold before anyone acts. The operator may need to expedite supply or use an approved substitute rather than rely on a routine purchase order.
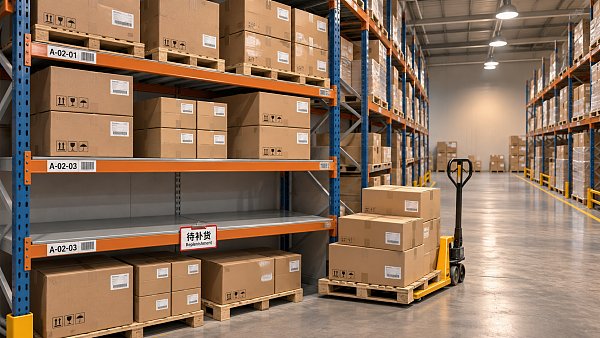
Choose an order quantity that fits the operating constraints
The reorder point says when to act; it does not determine how much to buy. Ordering too little can create repeated administrative work and freight charges. Ordering too much consumes storage space and cash, and increases exposure to damage, expiry, or obsolescence.
Fixed quantity or order-up-to target?
A fixed order quantity is practical when consumption is reasonably stable and suppliers deliver in standard batches. Each time the reorder point is reached, the buyer orders the same quantity, adjusted where necessary for minimum order quantities or pack sizes.
An order-up-to target is often easier when demand changes between reviews. The suggested order is the target stock position minus the current inventory position. For example, if the target is 600 units and the current position is 230, the initial recommendation is 370 units. A pack-size requirement, storage limit, or unreliable incoming shipment may justify a different final quantity.
When inventory is reviewed periodically rather than continuously, the target must cover expected demand over both the review interval and the replenishment lead time, plus an appropriate buffer. A weekly review followed by a two-week lead time exposes stock to demand for roughly three weeks after one review, not just two.
Where economic order quantity helps—and where it does not
Economic order quantity, or EOQ, provides a starting estimate when demand and costs are relatively stable:
EOQ = √(2 × annual demand × ordering cost per order ÷ annual holding cost per unit).
Ordering cost should reflect the relevant cost of placing and processing an order; holding cost may include financing, storage, insurance, and expected loss or obsolescence. Both are estimates, so the output should be treated as a decision aid rather than an instruction. EOQ is less reliable when demand is intermittent, prices change sharply, capacity is constrained, or expiry limits how long stock can be held.
Before releasing any suggested quantity, check supplier minimums, purchase multiples, freight breaks, available cash, shelf life, and warehouse capacity. A low unit price on a large order may be outweighed by the cost of stock that cannot be used or sold in time.
Size safety stock for variability, not habit
Safety stock protects against uncertainty in demand, lead time, or both. It should not become a permanent patch for inaccurate records or purchase orders that are routinely approved late. Those problems need separate correction; otherwise, the buffer grows while the underlying risk remains.
For an item with reasonably predictable daily demand variation and a fixed lead time, one common approximation is:
Safety stock = service factor × standard deviation of daily demand × √lead time in days.
This approach assumes, among other things, independent daily demand and an appropriate demand distribution. The service factor corresponds to a chosen cycle-service target: the probability of avoiding a stockout during a replenishment cycle, not the percentage of units filled from stock. If lead time is variable, the calculation needs to account for that variability too. For highly seasonal or intermittent demand, a simple formula may be misleading; scenario analysis or a model designed for intermittent demand may be more suitable.
The service target is a business choice. A low-cost fastener that can stop a production line may deserve more protection than an expensive item with readily available substitutes. Conversely, a short shelf-life product may require a lower buffer and more frequent replenishment. Record who approved the target and why, so the setting can be revisited when conditions change.
Handle exceptions before accepting the recommendation
A calculation based on historical averages can look reasonable while missing a known event. Before converting a recommendation into a purchase order, check the exceptions most likely to invalidate it:
- Demand changes: Confirm upcoming promotions, maintenance shutdowns, project starts, and confirmed large orders. Remove one-off anomalies from the baseline only when there is a documented reason.
- Supplier changes: Compare quoted lead time with actual receipt and release dates. Investigate repeated partial deliveries, late confirmations, or quality holds.
- Stock quality: Check whether damaged, expired, or quarantined units have been excluded from usable stock.
- Open orders: Confirm quantities and expected dates, especially when a late shipment is still counted as arriving on schedule.
- Item transitions: Review substitute parts, engineering changes, and planned discontinuations before replenishing an old specification.
For cross-border purchases, the lead-time review may also need to account for customs processing, transport handoffs, and inspection. These are reasons to examine the actual supply route, not to add an arbitrary number of days to every item.
Build a daily workflow around the decisions that need attention
A useful decision-support workflow begins with a clean exception queue. Group recommendations by urgency and consequence: items already below their reorder point, critical parts with uncertain incoming supply, and orders whose suggested quantity exceeds a normal limit. A long list of routine alerts makes it harder to spot the few that need judgment.
For each recommendation, the operator should be able to inspect the demand period used, current inventory position, lead-time assumption, safety stock, open orders, and the proposed quantity. If the number is overridden, capture a short reason such as “confirmed project demand” or “supplier delivery date revised.” That history helps distinguish a sound manual intervention from a recurring data problem.
After the order is placed, the work is not finished. Confirm the supplier’s acknowledgement, update the expected receipt date, and follow up on overdue lines. On receipt, record the quantity actually accepted and the date the material became usable. Those details improve the next lead-time calculation and reveal whether shortages originate in purchasing, transport, receiving, or inspection.
Review performance at an item or segment level using measures such as stockout frequency, service level, inventory age, and supplier delivery reliability. Investigate the reason behind a change rather than optimizing a single metric. Fewer stockouts achieved by accumulating obsolete material may not be an improvement.
Evaluate tools by the assumptions they expose
A spreadsheet may be adequate for a limited range of stable items if ownership, updates, and checks are clear. A larger operation may need inventory or supply chain software that connects demand, purchasing, warehouse transactions, and supplier data. In either case, ask whether users can adjust review intervals, distinguish usable from blocked stock, handle pack sizes, and see how suggested orders were calculated.
Automation is most valuable when data is reliable and exceptions have clear owners. It is less useful when it silently creates orders from outdated lead times or treats every open purchase order as certain. Test a proposed workflow against actual historical situations: a late supplier, a sudden demand spike, a partial receipt, and a specification change.
TradeNexus Pro, operating through chinaspecialmetal.com, covers supply chain software and broader industrial supply conditions that can inform this evaluation. Market and supplier intelligence can provide context, but replenishment settings still need to be verified against the organization’s own transaction records and operating constraints.
A practical next step is to select a small group of consequential items, validate their usable stock and actual lead times, and compare the existing reorder settings with recent demand. Document the exceptions before expanding the method. A recommendation that operators can explain and challenge is more useful than a precise-looking number no one knows how to trust.
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
 Nov 22, 2026Golmud's 60 MW Liquid Air Storage Project Uses Fully Domestic EquipmentGolmud's 60 MW Liquid Air Storage Project Uses Fully Domestic Equipment
 Nov 22, 2026Precision Engineering for Medical Devices: Tolerances and MaterialsPrecision Engineering for Medical Devices: Tolerances and Materials
 Nov 21, 2026EDF Acquires 1GWh Holloway Battery Storage Project in AustraliaEDF Acquires 1GWh Holloway Battery Storage Project in Australia
 Nov 21, 2026Choosing Carbon Steel Grades for OEM Machined Parts: Key FactorsChoosing Carbon Steel Grades for OEM Machined Parts: Key Factors
 Nov 20, 2026China’s First Virtual Power Plant Report Says Capacity Target Met EarlyChina’s First Virtual Power Plant Report Says Capacity Target Met Early
 Nov 20, 2026Choosing an OEM Heavy Equipment Manufacturer: Capabilities and Quality ChecksChoosing an OEM Heavy Equipment Manufacturer: Capabilities and Quality Checks
 Nov 19, 2026India Adds Record 8.4 GW of Open-Access Solar in First Nine Months of 2026India Adds Record 8.4 GW of Open-Access Solar in First Nine Months of 2026
 Nov 19, 2026B2B Intelligence for Green Energy: Finding New Market OpportunitiesB2B Intelligence for Green Energy: Finding New Market Opportunities
 Nov 18, 2026Global Solar Additions Hit Record in 2025, Forecast to Fall in 2026Global Solar Additions Hit Record in 2025, Forecast to Fall in 2026
 Nov 18, 2026Supply Chain Visibility for Supplier Management: How to Spot Delivery RisksSupply Chain Visibility for Supplier Management: How to Spot Delivery Risks
 Nov 17, 2026US Battery Storage Deployment Tops 200 GWh; 74 GWh Forecast for 2026US Battery Storage Deployment Tops 200 GWh; 74 GWh Forecast for 2026
 Nov 17, 2026Choosing a Solar Tracker for Ground-Mount PV: Site and Design FactorsChoosing a Solar Tracker for Ground-Mount PV: Site and Design Factors
 Nov 16, 2026US Polysilicon and Solar Product Tariffs and Import Price Floor Take Effect December 4US Polysilicon and Solar Product Tariffs and Import Price Floor Take Effect December 4
 Nov 16, 2026How Industrial Buyers Can Evaluate B2B Intelligence Reports on SuppliersHow Industrial Buyers Can Evaluate B2B Intelligence Reports on Suppliers
 Nov 15, 2026CATL Sets Tener Sodium Delivery Timeline, Targeting LFP on CostCATL Sets Tener Sodium Delivery Timeline, Targeting LFP on Cost
 Nov 15, 2026Electric Wheelchairs for Disabled Adults: Choosing the Right Fit and RangeElectric Wheelchairs for Disabled Adults: Choosing the Right Fit and Range
 Nov 14, 2026China Expects Clean Energy to Meet All New Electricity Demand by 2030China Expects Clean Energy to Meet All New Electricity Demand by 2030
 Nov 14, 2026Choosing a Digital X-Ray Detector Supplier: Compatibility and SupportChoosing a Digital X-Ray Detector Supplier: Compatibility and Support
 Nov 13, 2026Ecuador Sets Zero VAT and Currency Outflow Tax Rates for Solar and Storage EquipmentEcuador Sets Zero VAT and Currency Outflow Tax Rates for Solar and Storage Equipment
 Nov 13, 2026Choosing an OEM Machined Parts Manufacturer: Quality, Capacity and Lead TimesChoosing an OEM Machined Parts Manufacturer: Quality, Capacity and Lead Times
 Nov 12, 2026South Africa Registers 2 GW of New Solar PV Capacity in Q3 2026South Africa Registers 2 GW of New Solar PV Capacity in Q3 2026
 Nov 12, 2026Mexico Supply Chain Market Research: Nearshoring Opportunities and RisksMexico Supply Chain Market Research: Nearshoring Opportunities and Risks
 Nov 11, 2026US Senate Advances Bipartisan BAAJA Energy Permitting BillUS Senate Advances Bipartisan BAAJA Energy Permitting Bill
 Nov 11, 2026Inventory Management Decision Support: When and How Much to ReorderInventory Management Decision Support: When and How Much to Reorder
 Nov 10, 2026China's Trade Surplus Tops $1 Trillion Through October as Exports Rise 35.2%China's Trade Surplus Tops $1 Trillion Through October as Exports Rise 35.2%
 Nov 10, 2026Choosing Surgical PPE: Gowns, Gloves, Masks and Eye ProtectionChoosing Surgical PPE: Gowns, Gloves, Masks and Eye Protection
 Nov 09, 2026US Solar Imports Shift as Domestic Manufacturing Investment Reshapes Global TradeUS Solar Imports Shift as Domestic Manufacturing Investment Reshapes Global Trade