Custom Molded Rubber Pricing: What Drives Unit Cost and Tooling Fees?
A custom molded rubber price becomes reliable only when the quotation separates recurring piece cost from one-time development cost. Two parts with a similar outside shape can carry very different prices because the compound, molding method, tolerances, cavity count, inspection burden, and expected service conditions are different. A low unit quote can also be misleading when it excludes trimming, post-curing, inserts, packaging, or the trial work needed to stabilize the part.
The useful comparison is therefore not a single quoted number. It is the total cost of obtaining conforming parts at the required volume, delivered in a condition suitable for assembly. That requires reading both the unit-price assumptions and the tooling proposal behind them.
Start with the cost structure, not the quoted piece price
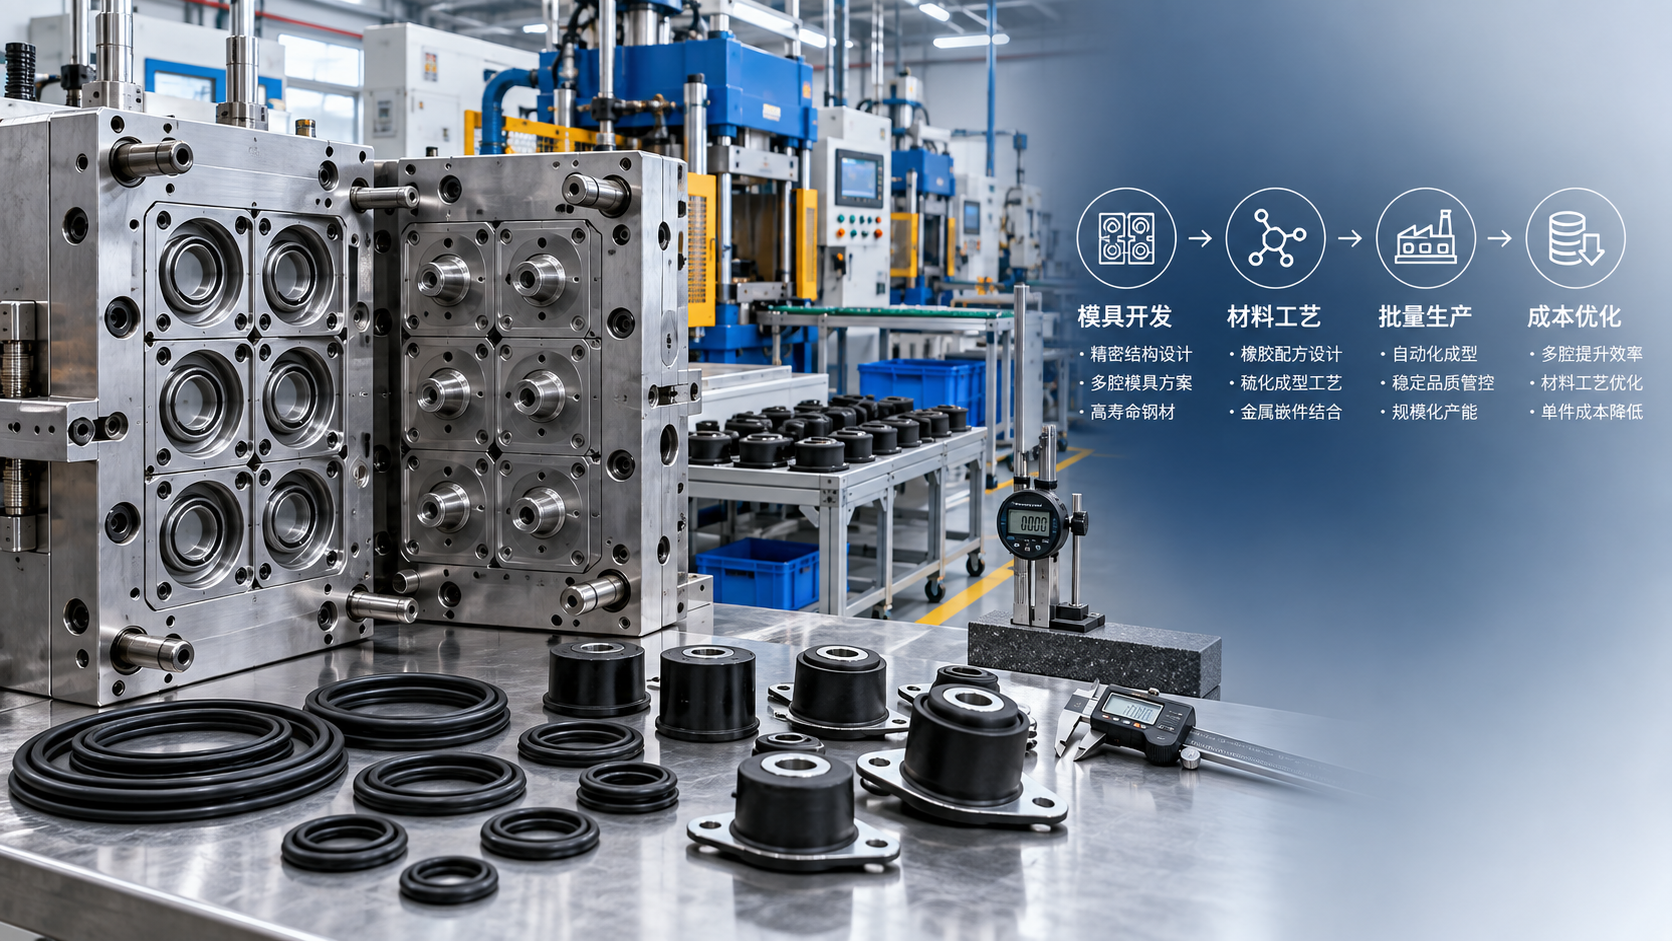
Most molded rubber quotations contain three cost layers. The first is variable cost: compound, molding-cycle time, labor, scrap, finishing, inspection, and packing. The second is semi-fixed production cost, such as setup, material batching, and lot-specific quality documentation. The third is non-recurring cost, which usually includes mold design, machining, sampling, revisions, gauges, and sometimes fixtures for secondary operations.
A small annual requirement often looks expensive per piece because setup and tooling recovery are spread across few parts. At higher quantities, the piece cost may fall sharply once a multi-cavity mold, automated handling, or reduced inspection time becomes viable. That decline is not automatic. If the component has a long cure cycle, difficult demolding, or a manual deflashing requirement, adding cavities may raise mold cost without creating a proportional reduction in labor.
Ask for the quotation to identify whether tooling is paid separately, amortized into the unit price, or retained by the molder. These commercial models can produce identical invoice totals in the first order while creating very different flexibility later. When tooling ownership, storage responsibility, maintenance expectations, and transfer rights are vague, a change of supplier can become more difficult than expected.
Material selection changes both resin cost and process behavior
Rubber compound cost is only one part of material-driven pricing. Natural rubber, EPDM, nitrile, neoprene, silicone, fluorosilicone, fluoroelastomer, and specialty compounds differ in raw-material value, but their behavior during mixing, curing, molding, and post-curing matters just as much. A compound selected for resistance to fuel, steam, ozone, refrigerant, high heat, low temperature, or cleaning chemicals may need longer processing time or more controlled handling.
Hardness alone does not define a compound. Two materials at the same nominal Shore hardness can differ in compression set, tear strength, volume swell, electrical properties, color stability, and cure response. A request that specifies only hardness and a generic material family leaves room for formulations that price differently and perform differently. A quote should tie the material to the actual duty cycle: media exposure, temperature range, pressure, UV exposure, intermittent versus continuous operation, and required service life.
Color also deserves attention. Standard black compounds are often simpler to source and process. White, translucent, bright-colored, or tightly controlled color parts may need dedicated mixing controls and heightened contamination prevention. Silicone parts used around sensitive assemblies may also require tighter limits on volatile residues or particulates, which adds process controls beyond the apparent simplicity of the geometry.
Compound approval should precede price optimization
Changing from a specified compound to a proposed equivalent can reduce quoted cost, but equivalence should be assessed against the installed condition rather than a short material data sheet. A static gasket, a dynamic seal, a vibration isolator, and a protective boot stress rubber in different ways. Compression, elongation, abrasion, fluid contact, and heat aging can expose weaknesses that are invisible in a basic hardness comparison.
When a substitute is being considered, request the proposed compound designation, relevant test values, and any known limitations tied to the application. This avoids a common source of later cost: a part that fits initial assembly but takes a permanent set, cracks after exposure, sticks to a mating surface, or loses sealing force over time.
Geometry determines mold complexity and production loss
Part volume influences material consumption, yet geometry often has a stronger effect on the molded rubber unit cost. Straightforward rings, pads, grommets, and flat seals can often be formed with relatively simple compression or transfer molds. Deep undercuts, thin unsupported sections, internal channels, variable wall thickness, sharp edges, and delicate lips introduce more demanding tool construction and a higher risk of damaged parts during release.
Flash is a useful example. A molded part normally develops excess material at the parting line, but the acceptable amount and removal method vary widely. Heavy flash on a nonfunctional exterior edge may be removed in bulk. A sealing edge, tiny port, or narrow groove may require hand trimming, cryogenic deflashing, precision tooling, or controlled inspection. The part may look simple in a drawing while its critical flash requirement makes it labor-intensive.
Parting-line location should be treated as a functional decision, not merely a tooling detail. Moving it away from a sealing surface can protect performance, but may require more complex mold construction. Likewise, an undercut may be manageable with flexible material and a carefully designed release angle, while another undercut requires inserts or collapsible tooling. The difference becomes visible in both tooling fees and cycle time.
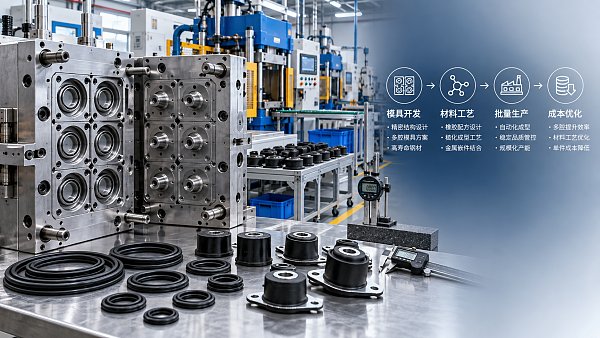
Metal inserts add another cost layer. The insert must be sourced or supplied, cleaned where necessary, accurately located, and retained during molding. Bonding rubber to metal also depends on preparation, adhesive systems, cure conditions, and validation of bond integrity. An insert with loose dimensional control can force the rubber molder to sort, fixture, or reject incoming pieces. The molded item then inherits variability that was not created in the rubber process.
Tolerances have a price only in relation to the molding state
Rubber is elastic, and dimensions change with temperature, post-cure behavior, material shrinkage, handling, and measurement method. Applying rigid-part tolerances indiscriminately often creates an expensive inspection regime without improving functional consistency. A narrow tolerance on a free, noncritical dimension may force unnecessary sorting. By contrast, a controlled compression dimension on a seal, a bore that locates over a shaft, or a thickness that determines electrical isolation may warrant focused control.
The drawing should identify datum logic and critical-to-function features. It should also state the condition in which dimensions are measured when that affects acceptance: free state, compressed state, assembled state, or after a defined conditioning period. A rubber part can appear out of tolerance when measured immediately after demolding yet stabilize within an agreed interval. Without an agreed measurement basis, inspection disagreements can generate avoidable returns and production holds.
Tooling fees reflect the production method selected
Tooling is not a generic entry fee. Its scope changes with compression molding, transfer molding, injection molding, liquid silicone rubber molding, and the use of secondary trimming or assembly fixtures. A basic prototype tool may prove shape and material behavior, while a production tool is built for repeatability, cavity balance, service life, and efficient loading. Treating the first as interchangeable with the second can create false savings.
Compression molds are commonly suited to many medium-volume elastomer parts and can be economical for larger shapes. They often require preforms or manually placed compound, so labor and part-to-part consistency deserve review. Transfer molding moves compound through channels into cavities and can offer better control for certain complex profiles or insert-molded parts, though runners create material loss. Injection molding may support efficient high-volume output, but the higher tool and process-development investment only makes sense when volume, geometry, and material behavior support it.
The number of cavities is a central tooling decision. More cavities increase output per press cycle, but they introduce questions about cavity-to-cavity variation, balancing, maintenance, inspection sampling, and the cost of a repair if one cavity is damaged. A single-cavity mold may be commercially sensible during design validation or for low, irregular demand. A higher-cavity tool is more attractive when demand is stable and the part has a predictable molding cycle.
Tooling proposals should state the cavity count, intended process, steel or construction approach where relevant, included trial rounds, sample quantity, and the boundary between normal adjustment and chargeable engineering changes. A fee that appears low may cover only the initial cavity machining, leaving fixtures, gauges, compound trials, or post-cure development as later additions. The purpose is not to eliminate all later charges; it is to distinguish design changes from costs that were foreseeable at quotation stage.
Volume breaks must match the actual release pattern
Quoted price breaks are useful only when they correspond to the way parts will be ordered and shipped. An annual forecast of a large quantity does not produce the same economics as numerous small releases if the supplier must repeatedly set up equipment, batch material, inspect first-off pieces, and pack short runs. Conversely, a large production batch may lower molding cost while increasing storage exposure, shelf-life management, and the risk that an engineering revision makes inventory obsolete.
Distinguish annual forecast, blanket-order quantity, minimum release quantity, and shipment quantity. These terms are often compressed into a single volume figure even though they allocate cost differently. Where demand is uncertain, a staged arrangement can reduce the risk of overcommitting to a high-cavity production tool before fit, material, and field conditions are established.
Secondary operations are frequently underestimated
Many pricing surprises appear after molding. Post-curing may be needed to stabilize certain compounds or reduce residual byproducts. Deflashing can range from simple tumbling to precise hand work. Washing, drying, applying lubricant, adhesive backing, printing marks, assembling clips, and packaging to prevent deformation all affect final cost. A soft seal packed under excessive compression can arrive permanently distorted even though it passed outgoing inspection.
Inspection requirements also need to be specific. A request for “100% inspection” has little meaning without defining the characteristics, measurement method, acceptance criteria, and recording requirement. Visual inspection for contamination differs from dimensional measurement of a critical groove, and both differ from leak testing an assembled component. Broad language encourages suppliers to include a contingency or assume a lighter level of verification than the application requires.
Comparing quotations without losing the technical basis
Normalize quotations before selecting the lowest figure. Put each offer against the same drawing revision, compound requirement, annual forecast, release schedule, incoterm, packaging definition, quality documentation, and tooling assumptions. Confirm whether the quoted unit cost includes scrap allowance, material certification where requested, first-article samples, post-cure, flash removal, and freight packaging. A supplier that asks detailed questions is often exposing an undefined requirement rather than making the process difficult.
Pay close attention to exclusions stated in broad terms such as “special inspection,” “material surcharge,” “tool modification,” or “customer-approved sample.” These are not automatically unfavorable clauses. They need a practical definition. For example, an engineering change after samples are approved should be treated differently from a mold correction required because the supplied tool did not meet the agreed drawing.
Lead time should be split into tooling lead time, sample-review time, material availability, production time, and shipping time. Combining them into one promise obscures where delays can occur. The same discipline applies to sample approval: specify whether approval is dimensional only, material-based, visual, assembly-based, or conditional on testing after environmental exposure.
A sound custom molded rubber price is one that remains traceable when the first production lot is released. Clear functional requirements, realistic tolerances, a defined compound, and transparent tooling scope reduce disputes more effectively than pushing for a lower headline number. The resulting quotation is easier to compare, easier to revise when demand changes, and less likely to transfer cost into rejected parts, delayed launches, or unplanned tool work.
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
 Oct 08, 2026How Digital Health Improves Diagnostic Accuracy and Workflow in Clinical LabsHow Digital Health Improves Diagnostic Accuracy and Workflow in Clinical Labs
 Oct 07, 2026Selecting Voice Picking Systems for German Warehouses: Integration, Languages and ROISelecting Voice Picking Systems for German Warehouses: Integration, Languages and ROI
 Oct 06, 2026How to Choose Last Mile Dispatch Software for On-Time Delivery at ScaleHow to Choose Last Mile Dispatch Software for On-Time Delivery at Scale
 Oct 05, 2026Vietnam’s Consumer Electronics Market: Demand Shifts and Sourcing OpportunitiesVietnam’s Consumer Electronics Market: Demand Shifts and Sourcing Opportunities
 Oct 04, 2026Digital Health Investment Priorities for Providers: Improving Access, Outcomes, and EfficiencyDigital Health Investment Priorities for Providers: Improving Access, Outcomes, and Efficiency
 Oct 03, 2026How to Specify an FR4 Custom PCB Board for High-Voltage and High-Heat DesignsHow to Specify an FR4 Custom PCB Board for High-Voltage and High-Heat Designs
 Oct 02, 2026ERP Software Market Intelligence: Adoption, Pricing, and Vendor Signals to WatchERP Software Market Intelligence: Adoption, Pricing, and Vendor Signals to Watch
 Oct 01, 2026How to Select Calibrated Temperature Data Loggers for GMP Cold Storage MonitoringHow to Select Calibrated Temperature Data Loggers for GMP Cold Storage Monitoring
 Sep 30, 2026Custom Molded Rubber Pricing: What Drives Unit Cost and Tooling Fees?Custom Molded Rubber Pricing: What Drives Unit Cost and Tooling Fees?
 Sep 29, 2026How to Evaluate Energy Management Software Vendors for Multi-Site OperationsHow to Evaluate Energy Management Software Vendors for Multi-Site Operations
 Sep 28, 2026How to Select a DIN Rail Smart Meter for Multi-Circuit Energy MonitoringHow to Select a DIN Rail Smart Meter for Multi-Circuit Energy Monitoring
 Sep 27, 2026TWS Earbuds in Vietnam: Demand Drivers, Price Tiers, and Retail Channel OpportunitiesTWS Earbuds in Vietnam: Demand Drivers, Price Tiers, and Retail Channel Opportunities
 Sep 26, 2026How UAE Clinics Can Qualify a Smart Glucometer Supplier for Accuracy and ComplianceHow UAE Clinics Can Qualify a Smart Glucometer Supplier for Accuracy and Compliance
 Sep 25, 2026Buying Aesthetic Lasers in the USA: FDA Status, Wavelengths, and Service SupportBuying Aesthetic Lasers in the USA: FDA Status, Wavelengths, and Service Support
 Sep 24, 2026Laser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin PartsLaser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin Parts
 Sep 23, 2026How to Choose Lightweight ANC Headphones for Comfortable All-Day TravelHow to Choose Lightweight ANC Headphones for Comfortable All-Day Travel
 Sep 22, 2026IPX5 TWS Bluetooth Earbuds: What Protection Do They Offer for Workouts?IPX5 TWS Bluetooth Earbuds: What Protection Do They Offer for Workouts?
 Sep 21, 2026What to Look for in a Grid Integration Company for Utility-Scale Solar ProjectsWhat to Look for in a Grid Integration Company for Utility-Scale Solar Projects
 Sep 20, 2026Microgrid Controller Pricing: What Drives Cost in Commercial Energy Projects?Microgrid Controller Pricing: What Drives Cost in Commercial Energy Projects?
 Sep 19, 2026How to Choose a GaN Charger for Laptops Without Compromising Power or PortabilityHow to Choose a GaN Charger for Laptops Without Compromising Power or Portability
 Sep 18, 2026Floating Solar Farm Costs: CAPEX, OPEX, and the Site Factors That Shape ROIFloating Solar Farm Costs: CAPEX, OPEX, and the Site Factors That Shape ROI
 Sep 17, 2026Drone Delivery Solutions for Last-Mile Routes: Site, Payload, and Range PlanningDrone Delivery Solutions for Last-Mile Routes: Site, Payload, and Range Planning
 Sep 16, 2026When Low-Volume Electronics Manufacturing Makes More Sense Than Mass ProductionWhen Low-Volume Electronics Manufacturing Makes More Sense Than Mass Production
 Sep 15, 2026Wholesale WiFi Smart Switches: What Buyers Should Verify Before OrderingWholesale WiFi Smart Switches: What Buyers Should Verify Before Ordering
 Sep 14, 2026How to Select IoT Sensors for Reliable Monitoring in Harsh Industrial EnvironmentsHow to Select IoT Sensors for Reliable Monitoring in Harsh Industrial Environments
 Sep 13, 2026How Procurement Teams Can Improve Supplier Reliability With Supply Chain VisibilityHow Procurement Teams Can Improve Supplier Reliability With Supply Chain Visibility
 Sep 12, 2026Smart Manufacturing Trends 2026: What Leaders Should Prioritize for ROISmart Manufacturing Trends 2026: What Leaders Should Prioritize for ROI