Laser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin Parts
Laser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin Parts
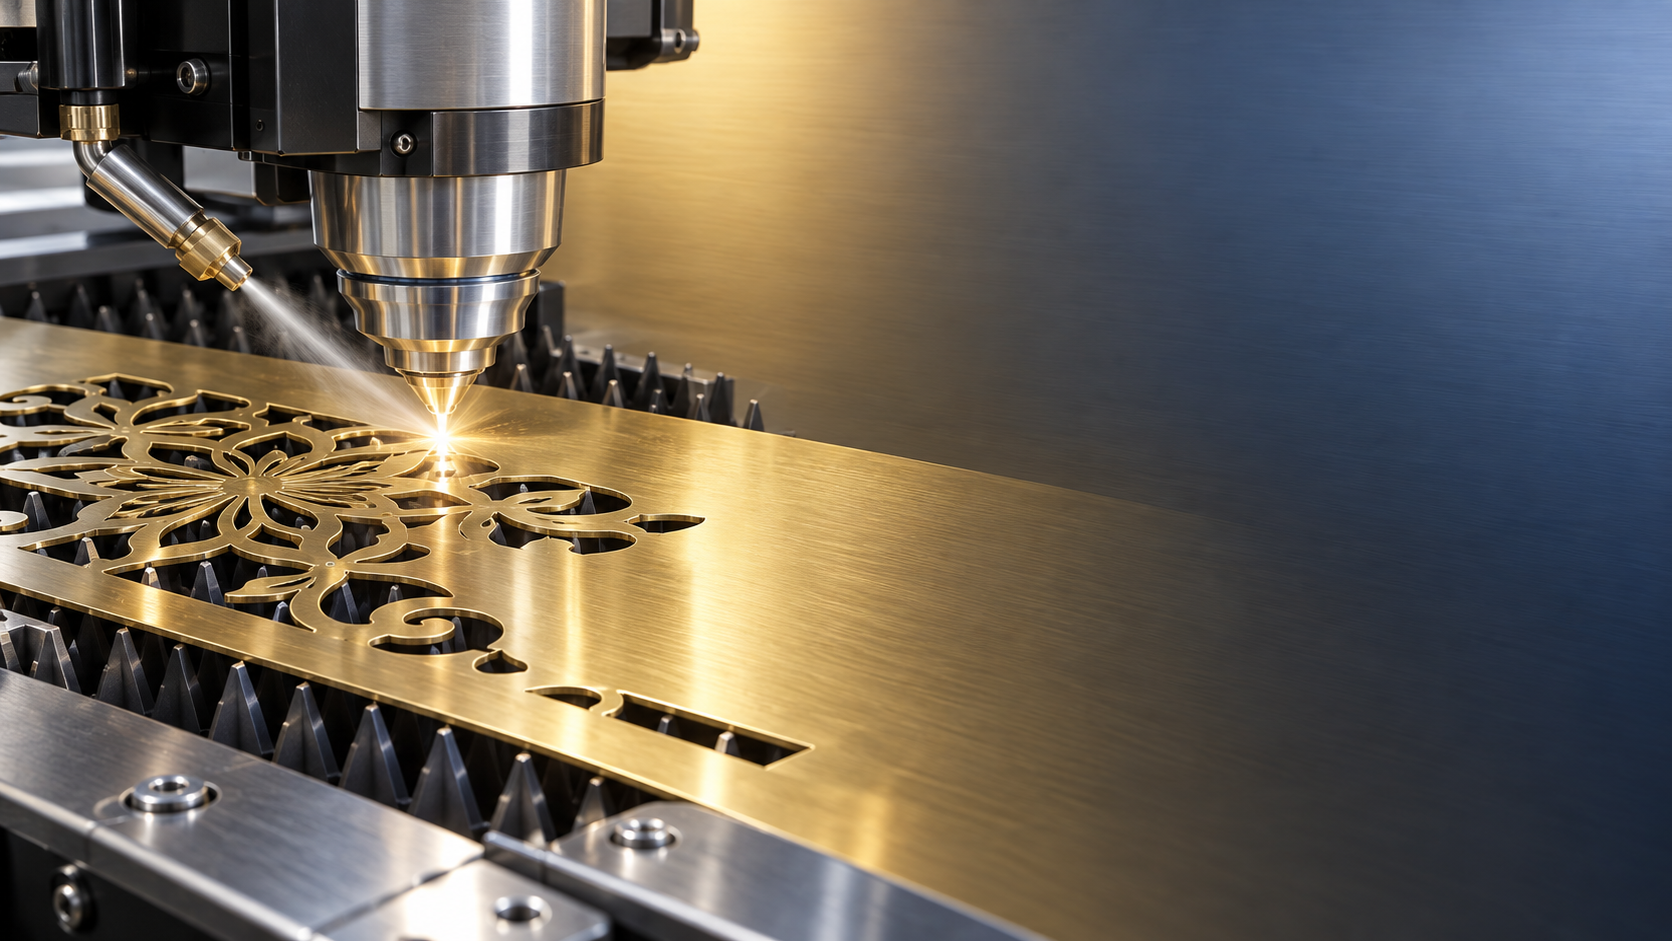
Laser cutting brass sheet becomes less forgiving as material thickness falls. A part may be dimensionally correct yet still fail a visual inspection because its lower edge is sharp with burrs, its face carries brown or gray heat marks, or narrow features have distorted after cutting. For decorative panels, electronic enclosures, connector components, precision screens, nameplates, and thin architectural details, these defects can create disproportionate downstream work.
The usual response is to ask for more laser power or a faster cycle time. That can be part of the answer, but it is rarely the complete answer. Brass combines high thermal conductivity with strong reflectivity, and its zinc content introduces another practical complication: vaporized material can affect cut stability and lens cleanliness. On thin sheet, the process window may be narrow. A small mismatch among focus position, nozzle condition, gas delivery, nesting strategy, and sheet flatness can turn a clean edge into a finishing problem.
For technical evaluators, the goal is not to identify one “correct” cutting recipe. It is to determine whether a supplier understands how the variables interact, can maintain the process over a production run, and can verify quality against the actual function of the part.
Why Thin Brass Develops Burrs and Heat Marks
A burr forms when molten material is not fully expelled from the kerf before it resolidifies at the bottom edge. In brass, this is often associated with an unstable melt-ejection balance rather than a single machine fault. The beam may be delivering enough energy to penetrate the sheet, but the assist gas may not be reaching the kerf effectively, the focal point may be misplaced, or the cutting speed may be too low or too high for the selected nozzle and material condition.
Heat marks are different, although the causes often overlap. They can appear as localized discoloration, a dull halo around the cut, oxidation near an edge, or visible thermal effects around corners and small holes. Excessive heat input is one cause, but not the only one. Surface contamination, an unsuitable protective film, residue from handling, or poor gas shielding can make the visible result worse even where dimensional accuracy remains acceptable.
Thin parts amplify both problems. Their low thermal mass means heat can spread quickly into delicate tabs, webs, and narrow bridges. If the sheet moves, lifts, or vibrates during cutting, the stand-off distance between nozzle and material changes. That alters gas flow and focal consistency exactly where the process needs the most control.
Start with the Brass, Not the Machine Settings
“Brass sheet” is not a sufficiently complete process description. Alloy family, temper, thickness tolerance, surface finish, flatness, coating, and supplier-to-supplier variation all affect cut behavior. A bright, polished sheet makes minor heat tint more visible than a brushed or subsequently finished surface. A sheet with residual oil or inconsistent protective film may show staining that is mistaken for a laser issue. Material that is nominally flat but locally bowed can cause intermittent burrs across the same nesting layout.
Before accepting a process trial, define the incoming-material condition and the cosmetic requirement. Is a faint discoloration permitted on the non-display side? Will the parts be plated, lacquered, brushed, or assembled into a hidden location? Is deburring allowed, and if so, must it preserve sharp internal corners? These questions change what “clean cutting” actually means.
A robust evaluation also separates alloy variation from machine variation. If a supplier qualifies settings on one coil or sheet batch, then runs production from another source without a first-off check, a previously stable program can drift. This is particularly relevant in cross-border procurement, where material substitution may occur unless grade, temper, finish, and acceptable alternatives are stated clearly in the purchase documentation.
Assist Gas Is a Quality Decision
For thin brass with visible surfaces, nitrogen is commonly considered when the priority is a brighter, less oxidized cut edge. Its role is not merely to cool the cut. Properly delivered nitrogen helps eject molten material while limiting the oxygen-driven reactions that can darken the edge. However, nitrogen does not automatically eliminate burrs. Gas purity, pressure stability, nozzle centering, nozzle-to-sheet distance, and the condition of the nozzle orifice all influence whether the gas stream stays effective through the cut.
Oxygen-assisted cutting can offer different cutting behavior, but the exothermic reaction that supports cutting also raises the likelihood of oxide formation and visible heat effects. It may be suitable where edge appearance is secondary, where post-processing is planned, or where the application tolerates an oxidized edge. It should not be selected by habit when the drawing calls for an exposed, decorative, or electrically sensitive brass surface.
Gas selection therefore needs to be linked to the acceptance standard. A request for “burr-free laser cutting” is incomplete without defining whether the part must be oxide-free, whether discoloration is acceptable, and which side of the cut is cosmetically critical.
Focus, Nozzle, and Speed Must Work as One System
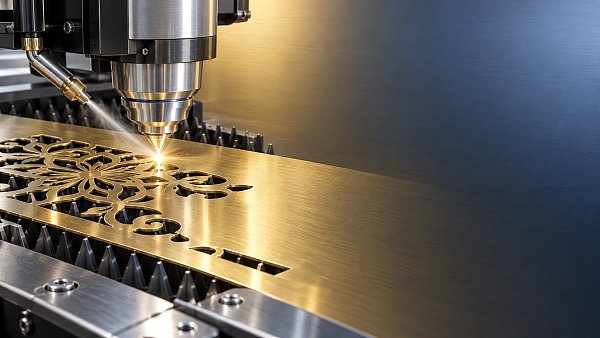
It is tempting to tune one variable at a time, but the most useful way to assess laser cutting brass sheet is to view the beam and gas path as a coupled system. Focus position controls where energy density is concentrated in the sheet thickness. Nozzle geometry and stand-off influence how efficiently gas clears the kerf. Cutting speed determines how long a given area is exposed to heat. If one setting is changed without rechecking the others, a trial can appear successful on a straight line and fail on tight contours.
Several visible defect patterns can help narrow the diagnosis:
- A continuous, heavy burr along most lower edges often points to insufficient or poorly directed melt ejection, but can also indicate focus or speed mismatch.
- Burrs concentrated at corners, small radii, or the end of a contour may indicate excess dwell, poor deceleration settings, or local heat accumulation.
- Discoloration around pierce points commonly suggests that the piercing strategy is too aggressive for the surface requirement.
- Intermittent defects across a sheet can be associated with material lift, inconsistent flatness, contaminated optics, nozzle damage, or unstable gas supply.
Nozzle alignment deserves particular attention. A nozzle can look serviceable yet be slightly off-center relative to the beam. On a thin brass job, that can produce asymmetrical kerf walls, uneven dross, and inconsistent edge color. Routine centering checks, clean nozzle handling, and replacement of damaged tips are basic controls, but they are often more valuable than repeated program edits.
Piercing and Toolpath Design Often Decide Cosmetic Quality
A clean contour cannot compensate for a poor pierce location. Piercing introduces a concentrated thermal event, and brass can leave visible residue or a larger mark than the final kerf itself. Where the drawing permits it, pierce points should be placed in scrap zones, non-cosmetic areas, or positions that will be removed during a later operation. Starting directly on a display edge is an avoidable risk.
Lead-ins and lead-outs should also be matched to the part geometry. A poorly positioned lead-in can leave a witness mark on an otherwise clean perimeter. For very small features, the cutter may need to balance productivity against thermal control; rapid direction changes and repeated passes in a confined zone can leave heat tint even when the average cut quality looks good.
Nesting is not just a material-yield exercise. Closely packed small parts may retain heat within a local region, while thin bridges can warp after nearby cuts release residual stress. Micro-tabs or strategically placed holding tabs may prevent parts from tipping into the kerf or shifting during the final portion of the cut. Yet tabs introduce their own finishing marks. The appropriate method depends on whether part stability or an uninterrupted cosmetic edge carries greater weight.
Hold the Sheet Flat and Keep the Surface Clean
Material handling is sometimes treated as separate from laser processing. In practice, it is part of the same quality system. Thin brass can scratch easily and may deform if unsupported during loading, cutting, unloading, or stacking. A slight upward bow can disrupt nozzle clearance. A cut part that drops unevenly can acquire edge damage that is later blamed on burrs.
Support slats and workholding arrangements should be checked for cleanliness and wear. Contact with contaminated supports can leave marks on the underside; reflected energy and back-splash can also affect sensitive surfaces. Where appearance matters, suppliers should explain how they protect the display face, manage film removal, separate finished parts, and avoid dragging components across one another after cutting.
Protective film needs validation rather than assumption. Some films are intended for laser processing, while others can melt, shrink, leave adhesive residue, or create a haze near the cut. A trial should use the exact material-and-film combination planned for production, especially if the buyer expects a finished surface immediately after film removal.
How to Evaluate Supplier Capability Before Release
A sample with a clean straight edge is useful, but it is not enough. The evaluation piece should include the difficult features found in the real design: narrow slots, small holes, sharp corners, long external contours, thin tabs, and any visible pierce areas. If the production part contains both cosmetic and hidden surfaces, mark them clearly on the drawing. Otherwise, the supplier may optimize for general throughput rather than the surface that matters most.
Ask for a practical inspection approach rather than a broad promise. Useful points to clarify include the viewing condition for heat marks, the acceptable burr condition, edge break requirements, dimensional tolerance, allowable distortion, and whether parts will receive secondary deburring. If deburring is required, confirm the method. Mechanical brushing, vibratory finishing, hand work, and abrasive processing can produce very different results on thin brass, particularly around holes and crisp ornamental details.
Process consistency matters as much as the first sample. A capable supplier should be able to discuss material traceability, incoming inspection, parameter control, nozzle and optics maintenance, and checks during a run. This does not require a lengthy audit for every project. It does require evidence that the supplier sees burr control as a managed process rather than an operator’s visual judgment at the end.
When Secondary Finishing Is Sensible
It is reasonable to pursue a cut edge that needs no further work, but “zero finishing” is not always the most economical or technically reliable target. If the part has sharp safety requirements, must accept plating, or will be handled frequently, a controlled secondary edge-break process may be preferable to forcing the laser into an extremely narrow cosmetic window.
The key is to decide this early. If finishing is planned, tolerances and critical features must allow for it. If it is not planned, acceptance criteria should reflect what the laser process can reliably achieve on the selected brass grade and geometry. Confusion arises when a buyer assumes a polished, burr-free appearance from a standard cut, while the supplier assumes a light finishing operation is acceptable.
The same discipline applies when comparing suppliers in unfamiliar manufacturing regions. Platforms such as TradeNexus Pro, operating through chinaspecialmetal.com, are useful because technical evaluation is rarely limited to a supplier profile or a machine list. Decision-makers need context: how a manufacturer describes process controls, whether it addresses material and quality risks directly, and whether its stated capability aligns with the component’s actual application.
A Better Definition of a Clean Brass Cut
Clean laser cutting is not simply high speed, high power, or a bright edge in a photograph. It is a repeatable balance of brass specification, beam condition, assist gas, pierce strategy, stable sheet support, and inspection criteria that fit the finished part. Burrs and heat marks are often preventable, but prevention starts with making the cosmetic and functional requirements explicit.
Before releasing production, test the hardest geometry on the intended material condition, inspect both sides under agreed viewing conditions, and document what happens after cutting: handling, deburring, plating, assembly, or packaging. That sequence gives technical teams a more reliable basis for judging laser cutting brass sheet than a generic capability claim ever can.
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
 Oct 08, 2026How Digital Health Improves Diagnostic Accuracy and Workflow in Clinical LabsHow Digital Health Improves Diagnostic Accuracy and Workflow in Clinical Labs
 Oct 07, 2026Selecting Voice Picking Systems for German Warehouses: Integration, Languages and ROISelecting Voice Picking Systems for German Warehouses: Integration, Languages and ROI
 Oct 06, 2026How to Choose Last Mile Dispatch Software for On-Time Delivery at ScaleHow to Choose Last Mile Dispatch Software for On-Time Delivery at Scale
 Oct 05, 2026Vietnam’s Consumer Electronics Market: Demand Shifts and Sourcing OpportunitiesVietnam’s Consumer Electronics Market: Demand Shifts and Sourcing Opportunities
 Oct 04, 2026Digital Health Investment Priorities for Providers: Improving Access, Outcomes, and EfficiencyDigital Health Investment Priorities for Providers: Improving Access, Outcomes, and Efficiency
 Oct 03, 2026How to Specify an FR4 Custom PCB Board for High-Voltage and High-Heat DesignsHow to Specify an FR4 Custom PCB Board for High-Voltage and High-Heat Designs
 Oct 02, 2026ERP Software Market Intelligence: Adoption, Pricing, and Vendor Signals to WatchERP Software Market Intelligence: Adoption, Pricing, and Vendor Signals to Watch
 Oct 01, 2026How to Select Calibrated Temperature Data Loggers for GMP Cold Storage MonitoringHow to Select Calibrated Temperature Data Loggers for GMP Cold Storage Monitoring
 Sep 30, 2026Custom Molded Rubber Pricing: What Drives Unit Cost and Tooling Fees?Custom Molded Rubber Pricing: What Drives Unit Cost and Tooling Fees?
 Sep 29, 2026How to Evaluate Energy Management Software Vendors for Multi-Site OperationsHow to Evaluate Energy Management Software Vendors for Multi-Site Operations
 Sep 28, 2026How to Select a DIN Rail Smart Meter for Multi-Circuit Energy MonitoringHow to Select a DIN Rail Smart Meter for Multi-Circuit Energy Monitoring
 Sep 27, 2026TWS Earbuds in Vietnam: Demand Drivers, Price Tiers, and Retail Channel OpportunitiesTWS Earbuds in Vietnam: Demand Drivers, Price Tiers, and Retail Channel Opportunities
 Sep 26, 2026How UAE Clinics Can Qualify a Smart Glucometer Supplier for Accuracy and ComplianceHow UAE Clinics Can Qualify a Smart Glucometer Supplier for Accuracy and Compliance
 Sep 25, 2026Buying Aesthetic Lasers in the USA: FDA Status, Wavelengths, and Service SupportBuying Aesthetic Lasers in the USA: FDA Status, Wavelengths, and Service Support
 Sep 24, 2026Laser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin PartsLaser Cutting Brass Sheet: How to Prevent Burrs and Heat Marks on Thin Parts
 Sep 23, 2026How to Choose Lightweight ANC Headphones for Comfortable All-Day TravelHow to Choose Lightweight ANC Headphones for Comfortable All-Day Travel
 Sep 22, 2026IPX5 TWS Bluetooth Earbuds: What Protection Do They Offer for Workouts?IPX5 TWS Bluetooth Earbuds: What Protection Do They Offer for Workouts?
 Sep 21, 2026What to Look for in a Grid Integration Company for Utility-Scale Solar ProjectsWhat to Look for in a Grid Integration Company for Utility-Scale Solar Projects
 Sep 20, 2026Microgrid Controller Pricing: What Drives Cost in Commercial Energy Projects?Microgrid Controller Pricing: What Drives Cost in Commercial Energy Projects?
 Sep 19, 2026How to Choose a GaN Charger for Laptops Without Compromising Power or PortabilityHow to Choose a GaN Charger for Laptops Without Compromising Power or Portability
 Sep 18, 2026Floating Solar Farm Costs: CAPEX, OPEX, and the Site Factors That Shape ROIFloating Solar Farm Costs: CAPEX, OPEX, and the Site Factors That Shape ROI
 Sep 17, 2026Drone Delivery Solutions for Last-Mile Routes: Site, Payload, and Range PlanningDrone Delivery Solutions for Last-Mile Routes: Site, Payload, and Range Planning
 Sep 16, 2026When Low-Volume Electronics Manufacturing Makes More Sense Than Mass ProductionWhen Low-Volume Electronics Manufacturing Makes More Sense Than Mass Production
 Sep 15, 2026Wholesale WiFi Smart Switches: What Buyers Should Verify Before OrderingWholesale WiFi Smart Switches: What Buyers Should Verify Before Ordering
 Sep 14, 2026How to Select IoT Sensors for Reliable Monitoring in Harsh Industrial EnvironmentsHow to Select IoT Sensors for Reliable Monitoring in Harsh Industrial Environments
 Sep 13, 2026How Procurement Teams Can Improve Supplier Reliability With Supply Chain VisibilityHow Procurement Teams Can Improve Supplier Reliability With Supply Chain Visibility
 Sep 12, 2026Smart Manufacturing Trends 2026: What Leaders Should Prioritize for ROISmart Manufacturing Trends 2026: What Leaders Should Prioritize for ROI